Industrial Applications of Polyurethane Rubber
The theoretical properties discussed earlier — high abrasion resistance, broad hardness range, strong load-bearing capacity — translate into a specific, well-defined set of industrial applications where polyurethane rubber has become the preferred material over conventional rubber or plastic alternatives. Understanding these applications in detail helps clarify not just where polyurethane rubber is used, but why it was chosen over the alternatives in each case.
Industrial Rollers and Wheels
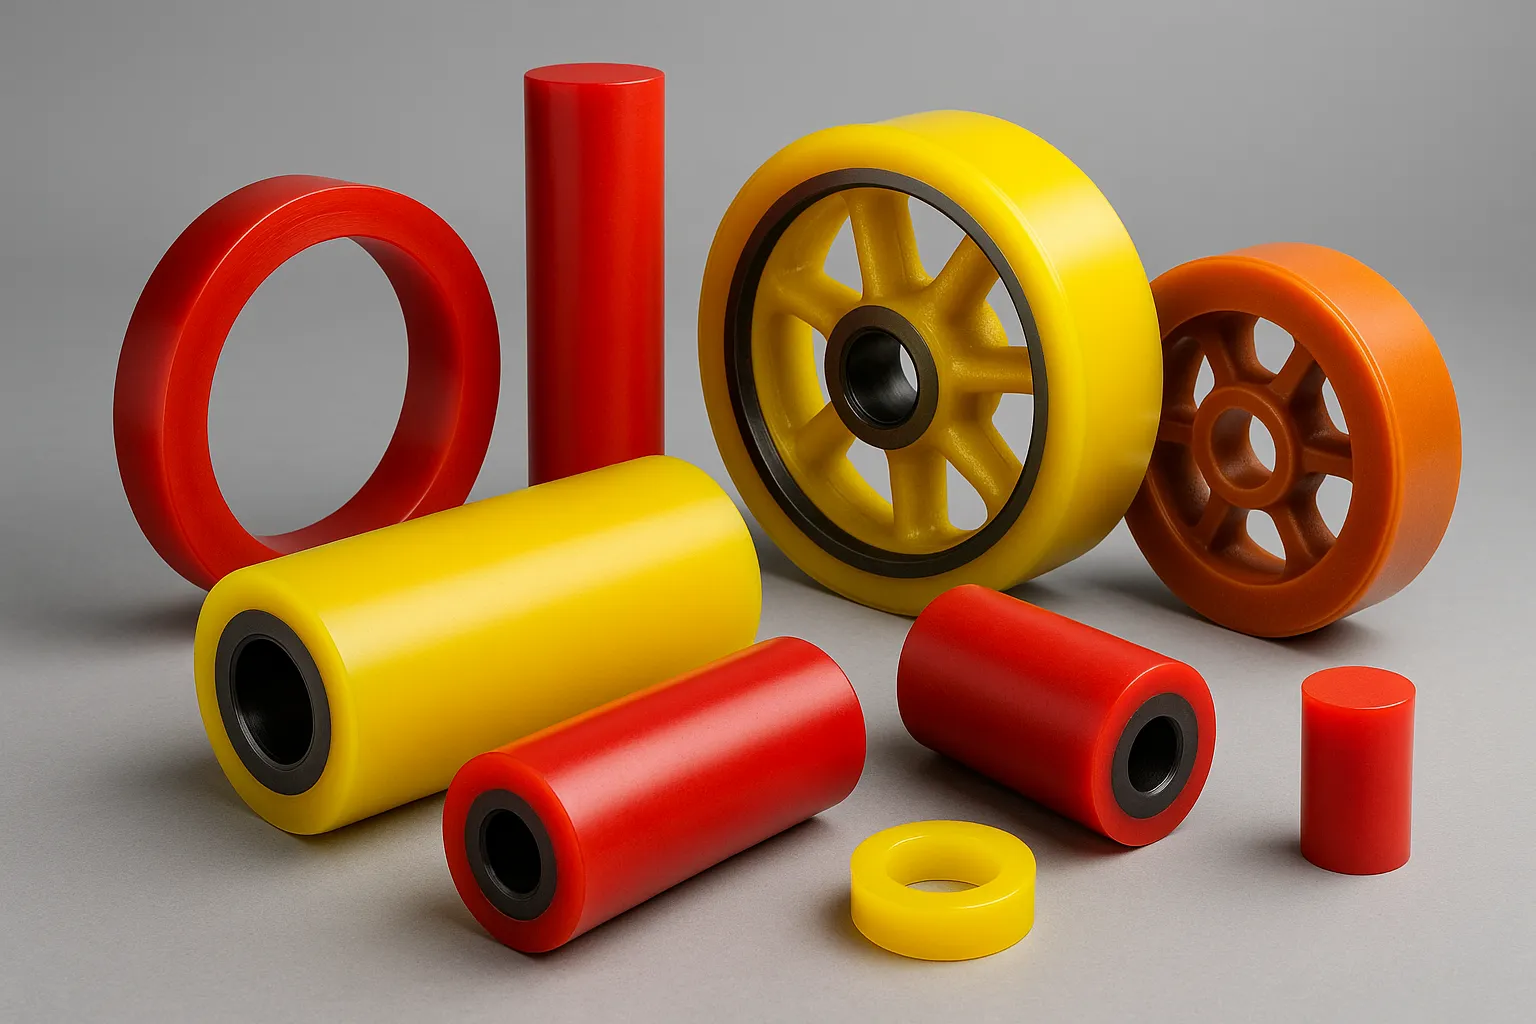
Rollers and wheels represent one of the largest and most established application categories for polyurethane rubber, spanning material handling, printing, conveyor systems, and automation equipment. In these applications, abrasion resistance, load capacity, and compression set behavior are the deciding factors, and polyurethane components consistently outlast rubber equivalents in abrasive conveyor and automation environments — a well-documented advantage across warehouse robotics, semiconductor automation, and general material-handling systems where particulate contamination and continuous wear are constant operating realities.
This performance advantage explains why polyurethane rollers are now found across an unusually diverse range of settings: conveyor and sortation systems in warehouses and distribution centers, printing and paper-processing equipment where dimensional consistency directly affects print quality, mining and heavy-duty conveyor operations, and port and logistics machinery handling continuous heavy loads. In each case, the underlying justification is the same — polyurethane’s combination of abrasion resistance and load-bearing capacity reduces the frequency of roller replacement compared to conventional rubber, directly reducing unplanned downtime in continuous-operation environments.
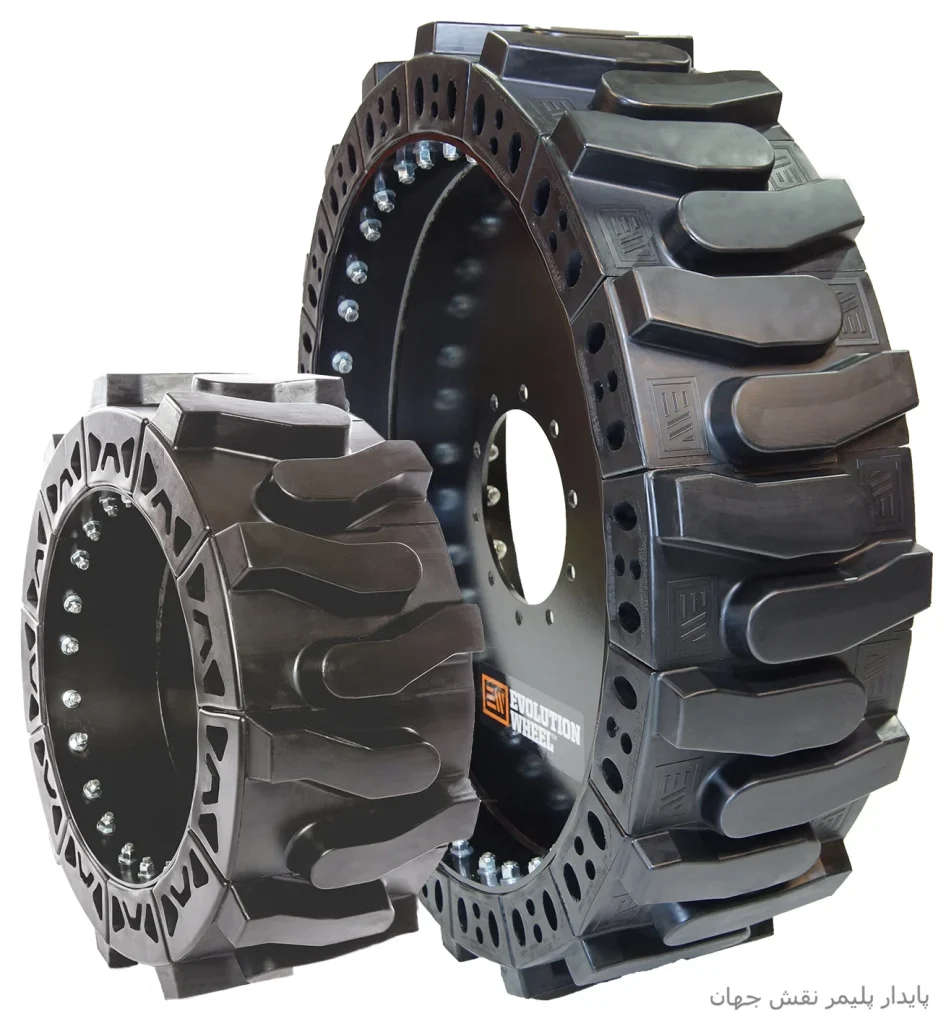
Forklift and Material Handling Wheels
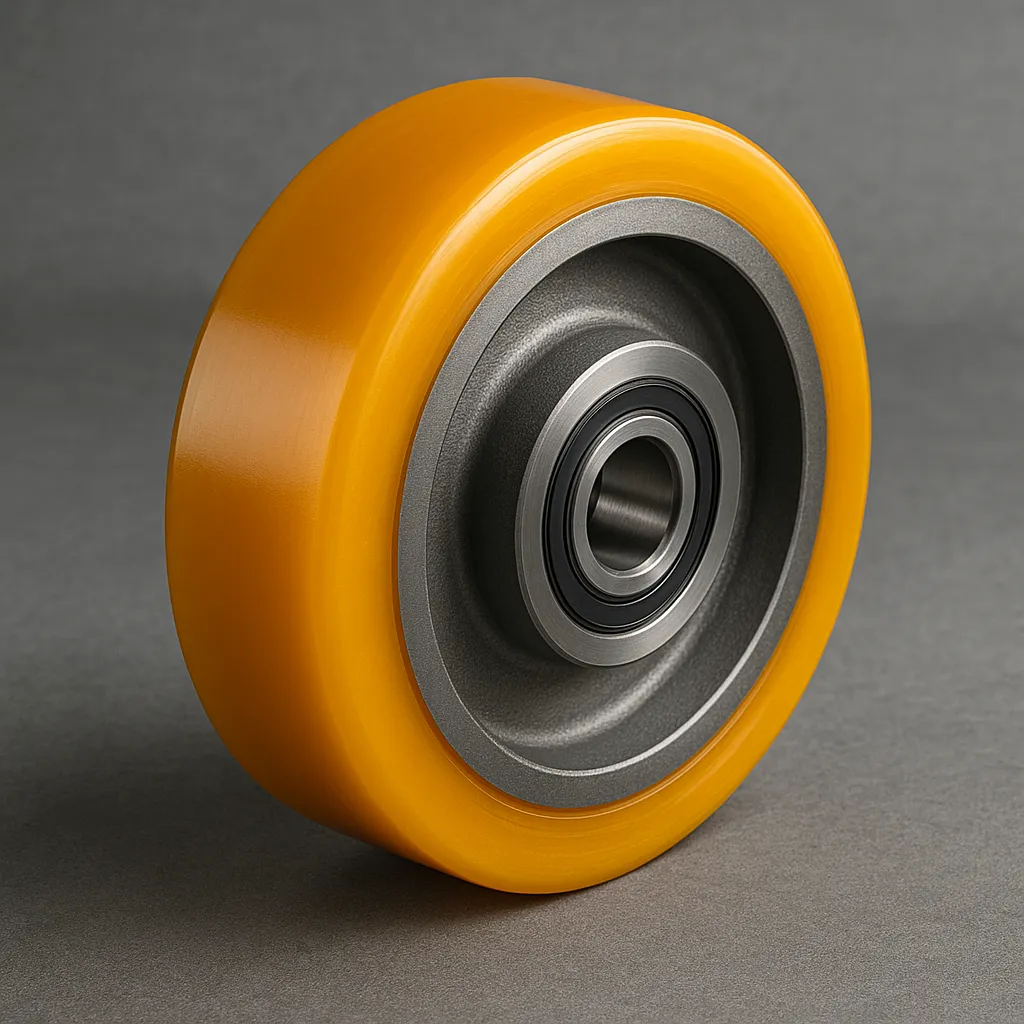
Solid polyurethane wheels have become the standard choice for forklifts, pallet trucks, and other material-handling vehicles operating on hard industrial floors. The rationale is straightforward: polyurethane’s high load-bearing capacity and abrasion resistance suit the repeated heavy loading and constant floor contact these wheels experience, while its resistance to cutting and gouging matters directly in warehouse environments where debris, metal shavings, or uneven surfaces are common.
An additional, often underappreciated benefit in this application is acoustic and vibration performance: polyurethane wheels generally offer better noise and vibration damping than metal wheels, while avoiding the rapid wear that plain rubber wheels experience under heavy, continuous industrial use — a combination that has made polyurethane the practical middle ground between the durability of metal and the cushioning of rubber.
Conveyor Belts and Belt Components
Beyond rollers themselves, polyurethane is also widely used in conveyor belt construction and related components, where cut resistance, flex fatigue resistance, and chemical tolerance are the properties that matter most for reliable long-term operation. Polyurethane belts typically deliver a combination of tensile strength and surface durability that rubber belts progressively lose as they age and fatigue under repeated flexing — a critical consideration in continuous-duty conveyor systems where belt replacement represents significant production downtime.
Mining and Heavy Industrial Equipment
The mining sector represents one of the most demanding application environments for any elastomer, combining constant abrasive wear from mineral particulates, heavy dynamic loading, and frequently harsh chemical or moisture exposure. Polyurethane rubber components — including pipe conveyor rollers, feed rollers, idler rollers, and various wear liners — are widely deployed specifically because standard rubber and plastic components tend to fail prematurely under this combination of stresses.
Oil and Gas Applications
In oil and gas environments, polyurethane’s resistance to hydrocarbon fluids becomes the primary selection driver rather than abrasion resistance alone. Polyurethane seals and gaskets are known to perform significantly longer in hydraulic, oil-and-gas, and chemical-processing environments compared to standard rubber seals, which tend to lose sealing force over time through thermal compression set under sustained heat and pressure exposure. This is directly connected to the chemical resistance properties discussed earlier — the reversible, minimal swelling polyurethane exhibits in hydrocarbon exposure translates into longer functional seal life under real operating conditions.
Printing and Textile Machinery
Precision and dimensional consistency are the deciding factors in printing and textile applications, where polyurethane rollers guide paper, film, and fabric substrates while maintaining even pressure distribution — directly affecting print quality and material handling accuracy. The same dimensional stability that makes polyurethane suitable for heavy mining loads also makes it suitable for the precision-tolerance demands of printing equipment, illustrating how the same underlying material properties serve very different application requirements depending on how the part is engineered.
Automotive and Impact-Absorbing Components
Polyurethane’s combination of impact energy return and dimensional stability makes it well suited to bumpers, mounts, and impact-absorbing components in automotive and automated guided vehicle (AGV) applications, where the material needs to absorb repeated impact while returning to its original shape rather than permanently deforming — a functional requirement that distinguishes structural impact components from simple cushioning applications.
Food Processing Equipment
For food-contact applications, specific FDA-compliant or equivalent food-grade polyurethane formulations are used in rollers and components exposed to wet and dry food-processing environments. This is an important practical distinction for buyers: standard industrial-grade polyurethane rubber is not automatically suitable for food contact, and food-grade certification must be explicitly specified and verified with the supplier rather than assumed.
Application Summary Table
| Application Area | Primary Property Driver | Why Polyurethane Rubber Is Selected |
|---|
| Conveyor rollers & wheels | Abrasion resistance, load capacity | Outlasts rubber under continuous abrasive wear |
| Forklift & material-handling wheels | Load capacity, cut resistance | Better floor contact durability than rubber |
| Conveyor belts | Cut & flex-fatigue resistance | Retains tensile strength longer than rubber belts |
| Mining equipment | Abrasion + chemical resistance | Withstands combined mineral abrasion and harsh exposure |
| Oil & gas seals/gaskets | Hydrocarbon resistance, compression set | Maintains sealing force longer under heat/pressure |
| Printing & textile rollers | Dimensional precision | Maintains consistent surface geometry over service life |
| Automotive/AGV bumpers | Impact energy return | Absorbs impact without permanent deformation |
| Food processing rollers | Food-grade compliance + wear resistance | Meets hygiene standards while resisting wet/dry wear |
A Note on Realistic Expectations
It is worth stating directly, rather than implying uncritically, that polyurethane rubber is not automatically the correct choice for every application within these categories. Selection still depends on matching the specific hardness, chemical formulation, and processing type (cast, TPU, or millable) to the actual operating conditions — a mismatched polyurethane grade can underperform a well-matched conventional rubber component in the same application. This is precisely why the selection framework discussed in the coming sections matters as much as the material family itself: Industrial Rubber performance in the field is ultimately determined by correct specification, not simply by choosing polyurethane over other elastomer options by default.
Polyurethane Rubber vs. Natural Rubber and Silicone: A Practical Decision Framework
Section two established the core technical differences between polyurethane rubber, natural rubber, and silicone. This section goes further, addressing the question buyers actually need answered: given a specific application, budget, and operating environment, which material delivers the better outcome — not in laboratory terms, but in real operating cost and service life.
Total Cost of Ownership, Not Just Purchase Price
One of the most consistent findings across industrial material comparisons is that initial purchase price is a poor proxy for total cost. The initial cost of a molded polyurethane part is often higher than a generic natural rubber equivalent, but this calculation shifts substantially once replacement frequency, labor costs for part swaps, and production downtime are factored in. In friction-heavy environments — mining, material handling, oil and gas — conventional rubber tends to shed material and lose structural integrity relatively quickly, while polyurethane’s superior abrasion resistance frequently translates into fewer replacement cycles and less accumulated downtime over the component’s operating life.
This does not mean polyurethane rubber is automatically the lower-total-cost option in every case — it means the comparison must be made on a service-life and downtime basis rather than unit price alone, particularly for components where replacement requires production stoppage.
Where Silicone Still Outperforms Polyurethane Rubber
Despite polyurethane’s advantages in abrasion and load-bearing applications, silicone remains the better technical choice in several specific circumstances that are worth stating clearly rather than glossing over:
- Extreme temperature environments. Silicone maintains flexibility and performance across a dramatically wider temperature range than standard polyurethane, making it the appropriate choice for applications involving sustained high heat, such as industrial ovens or certain automotive engine-adjacent components.
- Long-term UV and ozone exposure without aliphatic-grade formulation. As discussed in the properties section, standard aromatic polyurethane degrades faster under prolonged UV exposure than silicone, unless a more expensive aliphatic-isocyanate formulation is specifically selected.
- Medical, food, and high-purity applications. Silicone’s chemical inertness and long history of biocompatibility certification make it the default choice in many regulated medical and food-contact contexts, independent of mechanical performance considerations.
- Extreme flexibility with minimal compression set over very long service periods. Silicone’s elastic recovery under repeated, extreme deformation cycles is generally superior in applications that prioritize flexibility above wear resistance.
Where Natural and Synthetic Rubber Remain the Better Choice
Similarly, conventional rubber compounds continue to outperform polyurethane rubber in specific, well-defined scenarios:
- Low-cost, low-load general sealing and vibration damping, where the mechanical demands do not justify polyurethane’s higher unit cost.
- Applications requiring maximum flexibility at very low hardness, where conventional rubber’s elasticity profile is better suited than even the softest polyurethane grades.
- Cost-sensitive, high-volume commodity components where abrasion and load are not the dominant failure modes, and replacement cost is genuinely lower than the switching cost to a different material family.
A Practical Selection Checklist
Rather than defaulting to any single material based on general reputation, the following checklist reflects the accumulated reasoning from the technical comparisons above:
Common Mistakes When Comparing These Materials
Several recurring errors show up in real-world material selection decisions between these three elastomer families:
- Comparing materials at mismatched hardness levels. A soft-durometer silicone compared against a hard-durometer polyurethane will produce misleading conclusions about flexibility or abrasion performance; comparisons should always be made at comparable Shore hardness values.
- Assuming “polyurethane” implies uniform chemical resistance. As discussed earlier, polyester and polyether polyurethane formulations behave very differently in humid or hydrolysis-prone environments — treating all polyurethane rubber as chemically identical is a frequent and costly assumption.
- Ignoring total lifecycle cost in favor of unit price, particularly in high-replacement-frequency industrial settings where the cheaper part on paper often proves more expensive in aggregate operating cost.
This kind of application-specific, trade-off-aware comparison — rather than a blanket claim that one material is universally superior — is what distinguishes sound material specification in industrial rubber manufacturing from oversimplified marketing comparisons. Polyurethane rubber, natural rubber, and silicone each occupy a legitimate and well-justified place in industrial design; the goal is matching the material’s specific strengths to the specific demands of the component in question.
Polyurethane Rubber in Iran: Industry Landscape and Development Trends
Understanding how polyurethane rubber fits into Iran’s industrial landscape requires separating verified, documented facts from speculation. This section focuses strictly on what can be confirmed through the industry’s own public presence — its associations, established manufacturers, and the practical realities of raw material sourcing — rather than offering invented market figures or unverifiable growth statistics.
Organized Industry Structure
Iran’s polyurethane sector has developed a formal industry association structure, reflecting a maturing rather than emerging market. The Iran Polyurethane Manufacturers Association was established in 1399 (2021) by a founding board, and continues operating to represent and protect the interests and rights of its member companies. The existence of a dedicated national association — as opposed to polyurethane simply being a subcategory within a broader plastics or rubber trade group — is itself a meaningful indicator that the domestic industry has reached a scale where sector-specific coordination, standards discussion, and member representation are considered necessary.
Domestic Manufacturing Capability
Contrary to an assumption that polyurethane elastomers in Iran are exclusively imported, there is documented domestic production capability, including companies producing cast polyurethane elastomer raw materials to European-grade quality standards. One notable example is a company that, in collaboration with Iranian scientists, achieved industrial-scale production of these resin types and was recognized in 1394 (2015) as the first knowledge-based company in Iran’s polyurethane industry by the Presidential Office — indicating that domestic raw-material production, not just finished-part fabrication, has a documented track record rather than being a purely aspirational goal.
Beyond raw material producers, Iran also has an established base of companies manufacturing finished polyurethane rubber components — particularly industrial wheels and rollers — with product lines covering soft and hard abrasion-resistant wheels, rotating and fixed configurations, heavy-duty variants, and metal-cored designs. This finished-goods manufacturing layer indicates that the domestic value chain extends beyond raw material import and basic casting into more specialized, application-engineered product design.
Practical Realities for Iranian Buyers and Specifiers
For engineers and procurement teams working within Iran’s industrial sector, several practical considerations shape how polyurethane rubber is sourced and specified, based on the general structure of the domestic industry described above rather than any specific unverified claim:
- Raw material sourcing varies by supplier. Some Iranian polyurethane component manufacturers rely on domestically produced prepolymer and curative systems, while others may source raw chemical inputs internationally. This affects lead times, formulation consistency, and the ability to obtain specialized grades such as aliphatic (UV-stable) or food-grade formulations.
- Association membership can serve as a useful screening signal. Given that a formal manufacturers’ association exists, buyers evaluating potential suppliers can reasonably use association membership as one data point — among several — when assessing a supplier’s standing within the organized domestic industry, rather than as a substitute for direct technical qualification.
- Specialized grades may require more advance planning. As discussed earlier in this article, applications requiring specific formulation characteristics — food-grade compliance, aliphatic UV-stable chemistry, or high-hydrolysis-resistance polyether systems — are more specialized than general-purpose polyurethane rubber. Confirming a specific supplier’s capability to produce these grades, rather than assuming general availability, remains an important step in the specification process for any buyer, in Iran or elsewhere.
A Hypothetical Illustration of the Selection Process
To make this concrete without asserting unverified specifics: consider, hypothetically, an Iranian conveyor equipment manufacturer evaluating whether to specify polyurethane rollers instead of standard rubber rollers for a mineral-handling application. Following the decision framework outlined earlier in this article, the relevant considerations would include confirming the abrasive nature of the material being conveyed, verifying the roller supplier’s ability to provide a cast polyurethane grade suited to that abrasion profile, and weighing the higher initial component cost against the reduced replacement frequency expected in an abrasive operating environment. This is presented as an illustrative example of how the selection logic applies, not as a documented case study or verified project outcome.
Where Caution Is Warranted
It is worth being direct about the limits of what can be confidently stated here: precise figures on Iran’s polyurethane rubber market size, import-versus-domestic production ratios, sector growth rates, or pricing trends are not included in this article, because reliable, up-to-date, citable data on these specific figures was not available at the time of writing. Readers seeking current pricing or precise market-share data are encouraged to consult the Iran Polyurethane Manufacturers Association or individual manufacturers directly, since these figures shift with raw material costs and broader economic conditions in ways that would quickly outdate any number stated here as fact.
Selection Criteria for Choosing the Right Polyurethane Rubber for Each Application
Every principle covered so far — hardness range, chemical formulation, processing type, and application category — converges into a single practical question buyers and engineers ultimately have to answer: which specific polyurethane rubber grade is correct for this exact component? This section lays out a structured selection process rather than a generic recommendation list, since polyurethane rubber selection genuinely is less about identifying a single “best” material and more about systematically matching material behavior to real operating conditions.
Step One: Define the Dominant Failure Mode
Before any hardness or chemistry decision, the component’s actual failure history — or anticipated failure mode for a new design — should be identified. As discussed earlier, this failure-mode-first approach is more reliable than assuming polyurethane is a general upgrade over rubber in every dimension. Ask specifically: does the existing or comparable component fail through abrasive wear, cutting and tearing, compression set, chemical attack, UV degradation, or impact fatigue? Each failure mode points toward a different set of formulation priorities.
Step Two: Select the Appropriate Hardness (Durometer)
Hardness selection has the single largest impact on how a polyurethane rubber component performs, since it directly governs the balance between flexibility, load capacity, and abrasion resistance. Selecting too soft a durometer risks failure under load, while selecting too hard a durometer sacrifices the flexibility or cushioning the application may actually need.
The following reference points, drawn from established industry guidance rather than a single formula, illustrate how hardness typically maps to application type:
| Application Type | Typical Hardness Range | Rationale |
|---|
| Flexible seals, gaskets, cushioning | Shore 20A – 60A | High flexibility for conforming to surfaces and absorbing impact |
| General-purpose bumpers, feed rollers | Around Shore 60A | Balance of flexibility and durability |
| Mining screen panels, extreme abrasion surfaces | Shore 90A – 95A | Maximum abrasion resistance under continuous particulate wear |
| Forklift tires, heavy-load rollers | Shore 50D – 70D | High load-bearing capacity and tear resistance |
| Hard structural components, bumpers | Shore 60D and above | Minimal deformation under stress, near-rigid performance |
It’s worth noting explicitly that identical durometer readings do not guarantee identical performance across different formulations. Different underlying formulations can yield the same Shore hardness value while differing substantially in load-bearing capacity or tear strength — meaning hardness alone is never a sufficient specification. A supplier’s specific formulation, not just the durometer number, needs to be evaluated against the application’s mechanical demands.
Step Three: Match the Chemistry to the Operating Environment
With a hardness range identified, the next step is confirming the underlying polyol chemistry matches the environmental exposure the part will face — a decision covered in detail in the properties section of this article, but worth restating as a concrete checklist item:
- Wet, humid, or water-exposed environments → specify polyether-based polyurethane for superior hydrolysis resistance.
- Oil- or solvent-heavy environments with low moisture exposure → polyester-based polyurethane typically offers better solvent resistance.
- Sustained outdoor UV exposure → confirm aliphatic isocyanate chemistry rather than assuming standard aromatic-based polyurethane will hold up long-term.
- Extreme temperature swings → specify hardness and mechanical properties at the expected service temperature, not just at room temperature, and build in a safety margin for thermal extremes.
Step Four: Choose the Correct Processing Type
Referring back to the three processing families discussed earlier — cast, thermoplastic, and millable polyurethane — the production volume, part complexity, and mechanical severity of the application should determine which type is specified, rather than defaulting to whichever type a given supplier happens to stock. A heavy-load, custom-geometry mining roller and a high-volume standardized industrial wheel bushing call for genuinely different processing types, even if their hardness values happen to be similar.
Step Five: Account for Core Material and Bonding Requirements
For components such as rollers and wheels, the polyurethane layer is frequently bonded to a metal or rigid polymer core rather than being a solid polyurethane part throughout. This introduces an additional specification consideration: the bond strength between the polyurethane and core material under the expected load and shock conditions, and whether the core material itself (steel, aluminum, cast polymer) is appropriate for the application’s weight and corrosion requirements. Overlooking core-to-urethane bonding integrity is a common and often costly oversight, since bond failure — rather than polyurethane wear itself — is a frequent real-world cause of premature roller and wheel failure.
A Consolidated Selection Checklist
This systematic approach — moving from failure mode, through hardness, chemistry, processing type, and finally core/bonding considerations — reflects how experienced engineers actually approach polyurethane rubber specification in practice, rather than treating material selection as a single binary decision between “polyurethane” and “not polyurethane.”
Maintenance, Service Life, and Common Mistakes in Industrial Use
Even the correctly specified polyurethane rubber component can underperform its expected service life when maintenance, storage, or installation practices are inadequate. This final practical section addresses the operational side of polyurethane rubber — the factors that determine whether a well-selected material actually delivers the extended service life it was chosen for.
Understanding the Real Root Causes of Failure
A useful framework for thinking about polyurethane rubber failure separates root causes into three distinct categories, since failure investigations often focus disproportionately on the most visible cause while overlooking the other two:
- Incorrect specification — a component that was never suited to its operating conditions in the first place, which will fail even under perfect maintenance, because the underlying material choice was wrong from the start.
- Improper installation — issues such as incorrect bonding adhesive, misaligned mounting, or installation angles that create stress concentrations, allowing moisture or contaminants to reach areas the design never intended to expose.
- In-service degradation — the most visible failure mode, driven by contamination, lubrication issues, environmental exposure, or simple accumulated wear over time.
This distinction matters practically: a maintenance team troubleshooting premature polyurethane rubber failure should not assume the material itself is defective before ruling out specification and installation errors, since these are frequently the actual underlying cause even when the visible failure looks like ordinary wear.
Contamination and Lubrication: An Underappreciated Factor
For polyurethane rubber components operating in contact with lubricated machinery — rollers, bushings, and bearing-adjacent parts — contamination control has an outsized impact on service life. A substantial share of industrial wear across mechanical systems relates directly to lubrication management, with abrasive particle contamination in lubricants frequently triggering wear mechanisms independent of the load or duty cycle itself. Improving fluid cleanliness by even a modest degree has been shown to meaningfully extend the service life of hydraulic and mechanical components.
The practical implication for polyurethane rubber maintenance programs is clear: contamination control and correct lubricant selection — matched for viscosity, temperature, and elastomer chemical compatibility — are frequently the highest-leverage, lowest-cost actions available to extend component life, ahead of any material upgrade.
Environmental and Storage Considerations
Polyurethane rubber’s degradation pathways during both storage and service are driven by a consistent set of environmental factors: heat, light, oxygen, ozone, and humidity. These same factors were discussed earlier in the context of UV and hydrolysis resistance, but they apply just as directly to how finished parts and unused inventory should be stored and handled:
- Store finished parts in a dry, covered area away from direct sunlight — UV and heat exposure during storage can degrade a part before it is ever put into service.
- Avoid prolonged exposure to extreme temperature ranges during storage, since both very high and very low temperatures outside the recommended range can affect long-term material behavior.
- For liquid raw materials (prepolymer and curative systems), moisture exposure is a particular concern — atmospheric moisture can cause irreversible changes in liquid polyurethane components even before visible hardening occurs, which is why manufacturers typically specify limited shelf life for opened containers and recommend purchasing only the quantity needed within that window.
When these storage conditions are properly maintained, rubber and polyurethane products generally retain their properties without significant change for extended periods — meaning premature degradation in properly stored inventory is unusual and typically traceable to a specific storage lapse rather than inherent material instability.
Installation Practices That Extend Service Life
For bonded or mounted polyurethane rubber components — rollers on metal cores, bushings, mounted seals — correct installation practice has a direct and often underestimated effect on eventual service life:
- Install under proper load conditions. For components like bushings, tightening or seating fasteners only after the assembly is under its normal operating load prevents unintended pre-stress that can accelerate fatigue.
- Use compatible mounting and lubrication materials. Silicone-based or otherwise chemically compatible lubricants should be used where relevant, reapplied on a defined maintenance interval rather than left indefinitely, since dry friction accelerates surface wear regardless of the base material’s inherent abrasion resistance.
- Avoid aggressive cleaning methods. High-pressure washing directed at polyurethane rubber mounting areas can force water and contaminants into interfaces the design did not intend to be exposed, undermining otherwise sound installation.
Recognizing Early Warning Signs
Rather than waiting for complete component failure, a basic inspection routine — ideally folded into existing maintenance schedules rather than treated as a separate program — should watch for:
- Surface cracking or visible cutting damage, indicating abrasive wear exceeding the component’s design tolerance.
- Localized hardening, discoloration, or chalking, often associated with UV degradation in outdoor-exposed parts.
- Deformation or set under load that does not recover, suggesting compression set has exceeded acceptable limits for the application.
- Unusual noise or vibration in rollers or wheels, frequently an early indicator of bond failure at the core interface rather than bulk material wear.
A Realistic View of Service Life
It’s worth stating plainly that polyurethane rubber’s well-documented service life advantages over conventional rubber are not unconditional guarantees — they depend directly on correct specification, proper installation, and reasonable maintenance being in place simultaneously. A premium, correctly specified polyurethane rubber component installed incorrectly or left in a contaminated, poorly lubricated environment can still fail prematurely, sometimes faster than a properly maintained conventional rubber alternative. The extended service life polyurethane rubber is known for should be understood as the outcome of the entire chain covered across this article — correct material family, correct hardness and chemistry, correct manufacturing process, correct installation, and ongoing maintenance — not as an inherent, automatic property of the material name alone.
Conclusion: Bringing the Technical Picture Together
Polyurethane rubber occupies a genuinely distinct position among industrial elastomers — not as a universal replacement for natural rubber or silicone, but as a precisely engineered material family suited to a specific combination of demands: high abrasion resistance, strong load-bearing capacity, and a hardness range wide enough to bridge flexible rubber and rigid plastic in a single chemistry.
Throughout this guide, the recurring theme has been that polyurethane rubber’s real-world performance depends on getting several layered decisions right simultaneously, not on the material name alone. Hardness must match the load and flexibility profile of the application. Chemistry — polyester versus polyether, aliphatic versus aromatic — must match the moisture, chemical, and UV exposure the part will actually face. Processing type — cast, thermoplastic, or millable — must match production volume and mechanical severity. And once in service, correct installation and basic contamination control determine whether the material’s documented advantages in abrasion resistance and service life are actually realized in practice.
For engineers, procurement teams, and manufacturers evaluating polyurethane rubber for a new or replacement application, the practical takeaway is straightforward: start from the component’s dominant failure mode, work through the selection framework covered in this guide, and confirm the specific supplier’s formulation and processing capability against that framework — rather than treating “polyurethane rubber” as a single, interchangeable commodity material.
Frequently Asked Questions
What is the difference between polyurethane rubber and regular rubber?
Polyurethane rubber is a segmented polymer formed from a reaction between polyols and diisocyanates, while conventional or natural rubber is derived from a single-polymer latex chemistry. In practical terms, polyurethane generally offers a wider hardness range, higher abrasion resistance, and better resistance to oils and ozone than natural rubber, whereas natural rubber typically remains more cost-effective for low-load, general-purpose flexible applications.
Is polyurethane rubber stronger than natural rubber?
In terms of abrasion resistance, tear strength, and load-bearing capacity, polyurethane rubber generally outperforms natural rubber, particularly under sliding or impingement wear conditions. However, “stronger” depends on the specific property being compared — natural rubber can offer excellent elastic recovery and flexibility in applications where extreme abrasion resistance is not the primary requirement.
What is the difference between cast polyurethane and thermoplastic polyurethane (TPU)?
Cast polyurethane is a thermoset material formed through permanent chemical crosslinking, meaning it cannot be melted and reprocessed once cured. TPU, by contrast, is thermoplastic — its hard and soft segments are held together through physical rather than chemical bonds, allowing it to be melted and reprocessed using standard injection molding or extrusion equipment. Cast polyurethane generally offers higher performance in extreme-load applications, while TPU suits higher-volume, standardized part production.
How long does polyurethane rubber last in industrial use?
Service life varies significantly based on hardness, chemistry, application, and maintenance conditions, so no single figure applies universally. What can be said reliably is that, when correctly specified and properly maintained, polyurethane rubber components in abrasive or high-load environments typically outlast comparable natural rubber components, primarily due to superior abrasion resistance and load-bearing capacity. Actual service life should be evaluated case by case against the specific operating conditions rather than assumed from general industry claims.
Can polyurethane rubber be used outdoors?
Yes, but with an important caveat covered earlier in this guide: standard, lower-cost aromatic polyurethane formulations degrade faster under prolonged UV exposure than materials like silicone. For genuine long-term outdoor service, aliphatic isocyanate-based polyurethane formulations — specifically engineered for UV stability — should be specified rather than assuming any polyurethane grade will perform equally well outdoors.
Does polyurethane rubber resist oil and chemicals?
Generally, yes — polyurethane rubber offers meaningfully better resistance to oils, fuels, and many industrial chemicals compared to natural rubber, and this resistance is often reversible in nature rather than causing permanent degradation. However, chemical resistance depends heavily on the specific formulation, particularly whether a polyester or polyether-based polyol system is used, so the exact chemical environment should always be confirmed with the supplier for demanding applications.
What hardness of polyurethane rubber should I choose?
There is no single correct hardness — it depends entirely on the application’s failure mode and mechanical requirements. As a general reference, flexible seals and cushioning applications typically use softer grades (roughly Shore 20A–60A), general-purpose rollers and bumpers often use around Shore 60A, and heavy-load or extreme-abrasion applications such as forklift tires or mining screens typically require much harder grades, ranging from Shore 50D up to 90A–95A depending on the specific stress profile.